Manufacturers are expected to process increasingly diverse materials, maintain consistent quality, reduce waste, control energy consumption, and respond quickly to changing customer requirements. These expectations have made extrusion equipment an important part of modern production strategy.
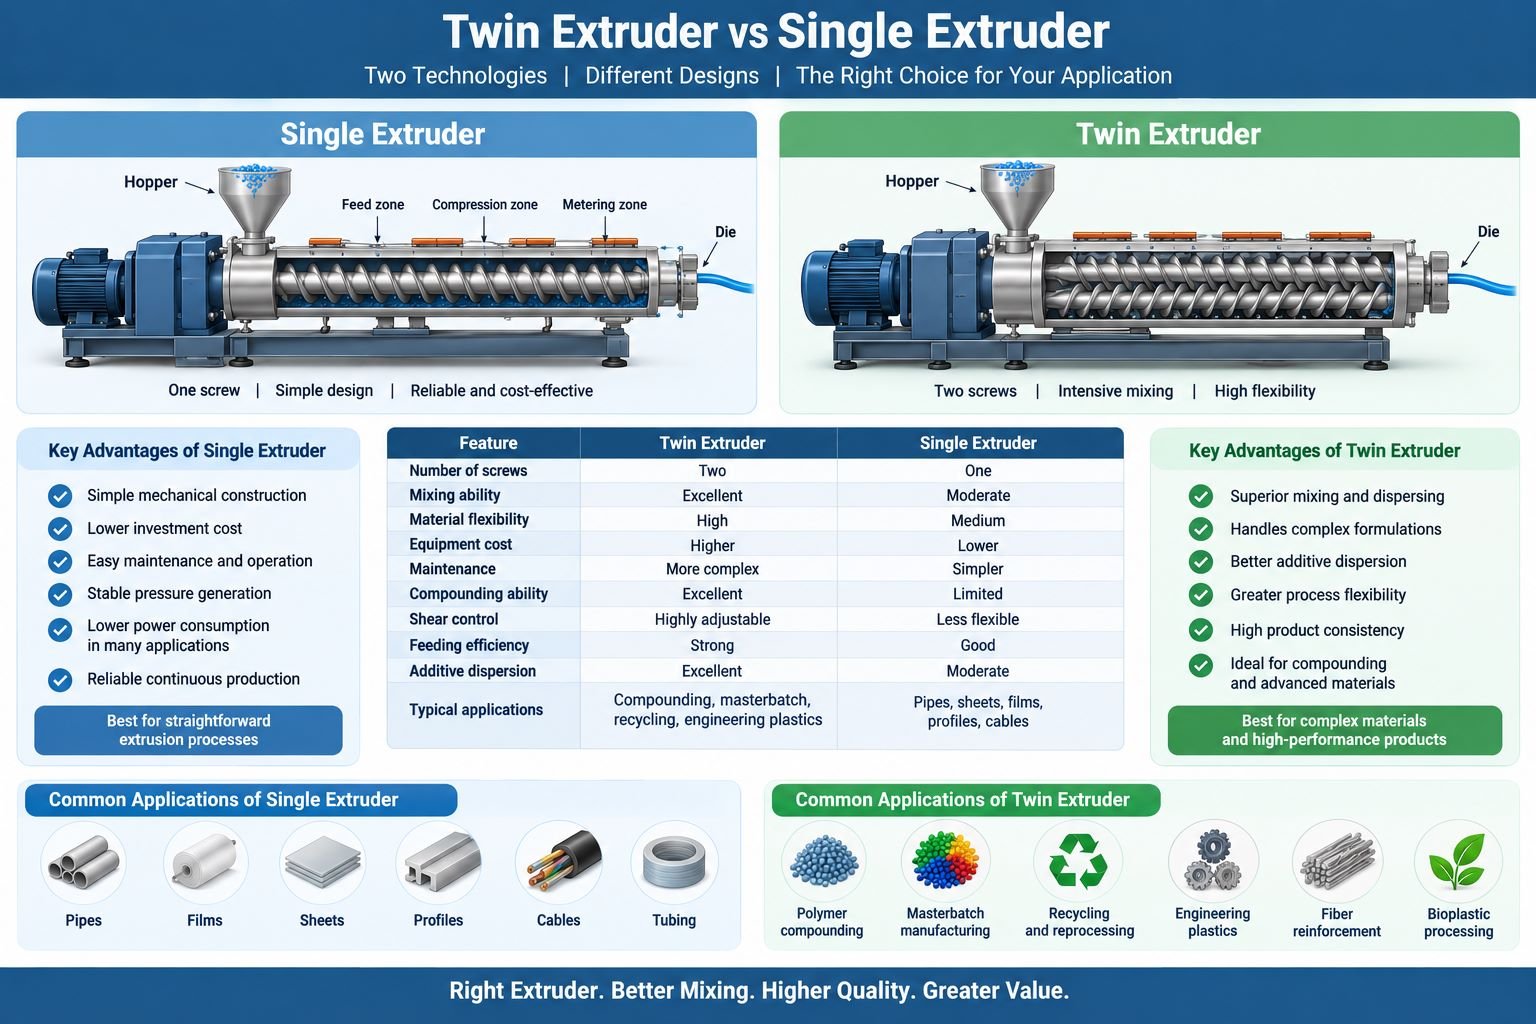
Among the technologies supporting this transformation are the twin extruder and single extruder. While both machines are designed for continuous material processing, their usefulness depends heavily on the production environment.
Instead of simply comparing the number of screws, manufacturers can gain more value by examining how extrusion equipment influences material flow, production stability, product consistency, and manufacturing flexibility.
Why Stable Extrusion Matters in Modern Manufacturing
A successful extrusion operation is not defined only by how much material a machine can process every hour.
Production must remain stable.
When an extrusion line experiences irregular feeding, temperature fluctuations, pressure variations, poor material preparation, or excessive equipment wear, the effects can appear in the finished product.
Manufacturers may experience dimensional variations, inconsistent color, surface problems, irregular pellets, higher scrap rates, or frequent production interruptions.
The objective should therefore be to create a predictable processing environment in which raw materials are transformed consistently.
Both the twin extruder and single extruder can contribute to this goal when correctly matched to the application.
Single Extruder Technology and Consistent Material Flow
A single extruder operates with one rotating screw inside a barrel. Raw material enters through the feeding section and is continuously carried forward.
As the material travels through the machine, heat supplied through the barrel combines with mechanical energy generated during screw rotation. The polymer gradually reaches the required processing condition before being delivered toward the die.
One of the strengths of this configuration is its straightforward continuous-processing principle.
For materials that do not require extensive ingredient incorporation, single-screw technology can provide stable melt delivery for products such as:
- Pipes
- Plastic profiles
- Sheets
- Films
- Tubing
- Wire insulation
- Cable coatings
In these production environments, maintaining consistent flow and pressure can be more important than providing highly intensive mixing.
Twin Extruder Technology and Formulation Control
The manufacturing challenge changes when the raw material contains multiple components.
For example, a polymer producer might need to combine resin with pigments, minerals, processing aids, stabilizers, reinforcing fibers, or functional additives.
Simply transporting these ingredients forward may not be enough. They need to be distributed under controlled processing conditions.
A twin extruder provides two rotating screws that can create a more configurable processing environment.
Depending on equipment design, screw elements can be selected to perform different tasks throughout the barrel.
This makes twin-screw technology particularly relevant for compounding, where the objective is to create a uniform material formulation rather than simply shape an existing polymer.
Material Feeding Can Determine Production Success
One area that receives less attention than screw design is feeding.
An extruder can only process material consistently when raw ingredients enter the system at an appropriate and stable rate.
Pellets generally behave differently from powders. Lightweight flakes can have different feeding characteristics from dense mineral fillers. Fibers introduce another set of challenges.
When several ingredients are used in one formulation, accurate feeding becomes even more important.
Modern extrusion lines may therefore use different feeding technologies depending on the raw material.
The extrusion process should be viewed as a coordinated system where feeders, screws, barrel sections, controls, dies, cooling equipment, and downstream machinery work together.
Temperature Is More Than a Heater Setting
Temperature control is another important part of extrusion performance.
Operators commonly control several barrel heating zones, but the displayed heater temperature does not necessarily represent the exact temperature of the polymer melt.
Mechanical shear generated inside the machine also contributes energy to the material.
Too little thermal energy can result in incomplete melting or unstable processing. Excessive heat can negatively affect heat-sensitive polymers or additives.
Successful extrusion therefore requires an appropriate balance between external heating, mechanical energy, screw speed, residence time, and material characteristics.
Both single extruder and twin extruder systems require careful temperature management.
Why Compounding Needs Greater Processing Control
Compounding is essentially the process of creating a modified polymer formulation.
A manufacturer might add calcium carbonate to achieve particular characteristics, pigment to develop a specific color, glass fiber for reinforcement, or processing aids to modify manufacturing behavior.
Each ingredient needs to become appropriately incorporated into the polymer.
This is where the configurable nature of a twin extruder becomes valuable.
Different sections of the screw arrangement can be designed for conveying, kneading, mixing, and other processing functions.
Additional feeding locations may also be used in suitable equipment configurations when certain ingredients should enter later in the process.
This level of flexibility supports applications such as masterbatch, engineering compounds, filled plastics, reinforced polymers, and specialized blends.
Production Efficiency Is Not Simply Maximum Speed
Running an extruder at the highest possible screw speed does not necessarily create the most efficient production process.
Efficiency should be measured according to usable output.
Consider the difference between producing 1,000 kilograms of material with a high rejection percentage and producing a slightly smaller quantity with almost all of it meeting specification.
The second operation may provide better commercial performance.
Useful extrusion efficiency indicators can include:
- Acceptable output per hour
- Scrap percentage
- Energy consumed per kilogram
- Production uptime
- Changeover duration
- Maintenance frequency
- Product consistency
- Labor requirements
Evaluating these factors creates a more realistic picture of extrusion performance.
Equipment Wear Should Be Included in Production Planning
Extruders operate continuously under demanding mechanical and thermal conditions.
Screws and barrels are exposed to friction, pressure, heat, and sometimes abrasive ingredients.
Materials containing significant quantities of certain mineral fillers or reinforcing components can create additional wear challenges.
As components wear, the internal processing characteristics of the machine can gradually change.
Manufacturers should therefore establish preventive maintenance schedules rather than waiting for production quality to deteriorate significantly.
Regular inspections of screws, barrels, gearboxes, heaters, sensors, feeders, and downstream equipment can help maintain predictable operation.
Twin Extruder and Single Extruder in Recycling
Recycled plastics are becoming an increasingly important part of polymer manufacturing.
However, recycled feedstock can introduce processing challenges because its characteristics may be less consistent than uniform virgin material.
Recycling operations can involve:
- Sorting collected plastic
- Removing unsuitable materials
- Washing the feedstock
- Grinding or shredding
- Drying
- Extrusion
- Filtration
- Degassing where appropriate
- Pelletizing
A single extruder can be suitable for certain prepared recycling streams, while a twin extruder can be useful when greater mixing, formulation modification, or additive incorporation is required.
The appropriate technology depends on the material rather than the recycled label alone.
Product Quality Begins Before Extrusion
One of the most common manufacturing mistakes is trying to solve every quality problem by adjusting the extruder.
Raw-material preparation can have an equally significant influence.
Moisture, contamination, incorrect ingredient ratios, particle-size variation, and inconsistent feedstock can all create processing problems.
Manufacturers should therefore establish quality controls before material enters the machine.
This may include raw-material inspection, drying, blending, weighing, controlled storage, and accurate dosing.
Stable input creates a much stronger foundation for stable extrusion.
Making an Extrusion Line More Flexible
Manufacturers rarely produce exactly the same products forever.
New customers may request different colors, higher filler percentages, recycled content, improved performance, or completely new polymer grades.
Production flexibility should therefore be considered during equipment selection.
A business focused primarily on straightforward continuous extrusion may find that a single extruder provides the necessary production capability without excessive complexity.
A compound manufacturer expecting frequent formulation changes may place greater value on the configurable processing options available through a twin extruder.
Future requirements can be just as important as current production demands.
Frequently Asked Questions
1. Why is extrusion stability important?
Stable extrusion helps manufacturers maintain consistent output, product dimensions, appearance, and material characteristics.
2. What does a single extruder do?
A single extruder uses one screw to continuously convey and process suitable material through a barrel.
3. Why is a twin extruder useful for compounding?
Its two-screw configuration provides greater flexibility for mixing and processing formulations containing multiple ingredients.
4. Does feeding affect extrusion quality?
Yes. Irregular material feeding can cause variations in output, pressure, formulation ratios, and finished-product quality.
5. Why is temperature control necessary?
Correct temperature management helps maintain appropriate material flow while reducing the risk of processing problems or thermal degradation.
6. Can single-screw extrusion handle recycled plastics?
Yes, depending on feedstock preparation, polymer characteristics, contamination, and final production requirements.
7. What causes extruder wear?
Mechanical friction, operating conditions, processing time, and abrasive materials can contribute to screw and barrel wear.
8. Is maximum screw speed the best production setting?
Not necessarily. The appropriate speed should provide stable processing and acceptable product quality.
9. Why are twin extruders used for masterbatch?
Masterbatch production often requires controlled distribution and dispersion of concentrated pigments, fillers, or additives.
10. How can manufacturers improve extrusion efficiency?
They can focus on raw-material consistency, stable feeding, optimized process parameters, preventive maintenance, operator training, and appropriate equipment selection.